

Microstructure, Oxide Film Behavior, and Advanced Shape Control Strategies
In modern hot strip rolling production, roll performance directly determines rolling stability, strip surface quality, shape accuracy, and overall cost efficiency. Compared with traditional indefinite chill cast iron (ICCI) rolls و high-chromium cast iron rolls, درافيل من الفولاذ عالي السرعة have become a mainstream choice for finishing stands due to their outstanding hot hardness, wear resistance, and thermal fatigue resistance.
The extended roll campaign brought by high-speed steel rolls delivers clear economic benefits, including reduced roll consumption and fewer roll changes. However, their application also introduces new technical challenges, particularly in oxide film evolution, thermal crown fluctuation, and strip shape control. If not properly managed, these issues may negatively affect surface quality and flatness stability.
This article provides an in-depth, engineering-oriented analysis of high-speed steel rolls in hot strip rolling, focusing on material microstructure, oxide film behavior, strip shape evolution mechanisms, and proven advanced control strategies from industrial practice.
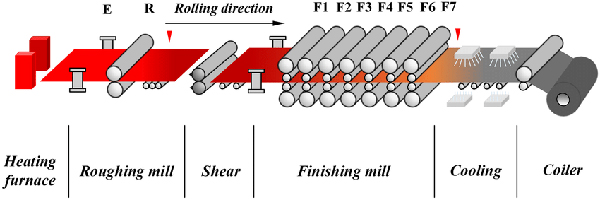
Material Characteristics and Microstructure of High-Speed Steel Rolls
High-speed steel rolls derive their superior performance from a highly alloyed chemical composition. Typical alloying elements include vanadium (V), chromium (Cr), molybdenum (Mo), tungsten (W), and niobium (Nb), all of which are strong carbide-forming elements.
Types and Distribution of Carbides
The working layer of high-speed steel rolls contains multiple types of hard alloy carbides embedded in a martensitic or tempered martensitic matrix.
MC-type carbides (mainly VC)
These carbides exhibit extremely high hardness, typically 2800–3000 HV, and are finely dispersed in granular form. They play a dominant role in improving wear resistance and maintaining surface roughness stability during long rolling campaigns.
M₂C, M₇C₃, and M₆C carbides
These carbides usually appear in network-like or herringbone distributions. They reinforce the matrix against high-temperature plastic deformation and improve resistance to thermal softening and surface fatigue.
The combined effect of these carbides allows high-speed steel rolls to maintain consistent performance under severe hot rolling conditions.
Key Physical Properties
Compared with conventional rolls, high-speed steel rolls generally exhibit:
-
Higher thermal conductivity
-
Larger coefficient of thermal expansion
-
Higher elastic modulus at elevated temperatures
These properties enable rapid heat transfer from the roll surface into the roll body, which improves thermal crack resistance. However, they also result in more pronounced and faster thermal crown development, especially during the initial rolling phase.
Oxide Film Formation, Evolution, and Delamination Mechanisms
Under hot rolling conditions characterized by high temperature, high contact pressure, and intensive water cooling, a spontaneous oxide film forms on the surface of high-speed steel rolls. This oxide film plays a decisive role in strip surface quality and rolling stability.
Protective Function of the Oxide Film
Under ideal conditions, a dense, uniform, and elastic black oxide film, mainly composed of Fe₃O₄, develops on the roll surface. This film provides multiple benefits:
-
Friction reduction
The oxide layer lowers the friction coefficient between the strip and the roll, reducing rolling force and energy consumption. -
Thermal insulation
The oxide film limits instantaneous heat flux into the roll body, mitigating thermal shock and delaying the initiation of thermal cracks (crazing). -
Prevention of metal adhesion
The film acts as a physical barrier, preventing direct high-temperature contact between the roll substrate and the steel strip, thereby avoiding sticking and pickup defects.
Oxide Film Delamination and Surface Defects
As rolling continues, the oxide film gradually thickens. Once its thickness exceeds approximately 5 μm, the film becomes prone to cracking and peeling.
Primary causes of oxide film delamination include:
-
Thermal expansion mismatch between the oxide layer and the roll substrate
-
Cyclic thermal stress induced by alternating heating and water cooling
-
Local stress concentration under high rolling pressure
Impact on strip surface quality:
-
Detached oxide fragments may be pressed into the strip surface, forming scale-in defects
-
Exposed roll substrate leads to uneven friction conditions, resulting in surface roughness variation and localized strip defects
Influence of High-Speed Steel Rolls on Strip Shape Control
Strip shape control in hot rolling mainly involves crown control and flatness control. The use of high-speed steel rolls significantly increases the complexity of shape prediction models.
3.1 Rapid Thermal Crown Fluctuation
Due to their high thermal expansion coefficient, high-speed steel rolls experience rapid diameter growth during the warm-up phase of rolling. Because heat is quickly conducted into the roll core, the thermal crown reaches its peak in a very short time, often before shape control systems fully stabilize.
This phenomenon is a major cause of strip shape fluctuation at the beginning of a rolling campaign.
3.2 High Stability of the Wear Profile
High-speed steel rolls exhibit extremely low wear rates. In typical hot strip mill operations, their wear depth may be only 20–30% of that observed in traditional rolls.
While this provides excellent long-term profile stability, it also eliminates the possibility of self-compensation through wear. Any initial roll profile prediction error may persist throughout the entire rolling campaign, making accurate modeling essential.
Advanced Application and Optimization Strategies
Practical experience from advanced hot rolling lines, such as the Shougang Jingtang 1580 hot strip mill, demonstrates that the challenges associated with high-speed steel rolls can be effectively managed through systematic process optimization.
4.1 Oxide Film Control and Maintenance Technologies
Cooling system optimization
Segmented cooling strategies and optimized nozzle angles are applied to ensure uniform roll surface temperature, reducing thermal stress and oxide film cracking.
Inter-stand lubrication
High-efficiency rolling oils are used to form a stable lubricating film, lowering frictional heat and suppressing excessive oxide film growth.
Water quality management
Strict control of cooling water pH and impurity content minimizes chemical corrosion and stabilizes oxide film adhesion.
4.2 Residual Thermal Crown Prediction and Compensation
Accurate prediction of the initial roll shape is the core solution for controlling early-stage strip shape deviation.
Residual heat calculation
Cooling time, ambient temperature, and roll history are recorded after roll removal. Finite element models or validated empirical models are used to calculate residual thermal crown before reinstallation.
Dynamic compensation strategy
Residual thermal crown values are introduced into secondary and tertiary shape control systems. During early rolling, systems automatically adjust work roll bending, CVC, PC settings, or reduction distribution to compensate for thermal expansion effects.
4.3 Variable Contact Length Rolling and Scheduling Optimization
To avoid localized fatigue damage and oxide film peeling, a coffin-shaped rolling schedule is adopted. Strip width is arranged from narrow to wide and then back to narrow, evenly distributing thermal load and contact stress across the roll face.
This strategy effectively prevents rib fatigue, improves oxide film stability, and extends roll service life.

Economic and Environmental Benefits
The application of high-speed steel rolls is not only a technological upgrade but also a key component of green and sustainable manufacturing:
-
Roll consumption reduced by over 50%
-
Significantly fewer roll changes, improving mill availability
-
Lower energy consumption across the roll life cycle
-
Reduced carbon footprint from roll manufacturing, grinding, and logistics
The successful industrial application at Shougang Jingtang’s 1580 hot strip mill confirms that, through precise thermal crown compensation and scientific oxide film management, the inherent challenges of high-speed steel rolls can be fully overcome.
مجموعة LMM One stop solution for steel mill

 Arabic
 English
 Russian
 Hindi